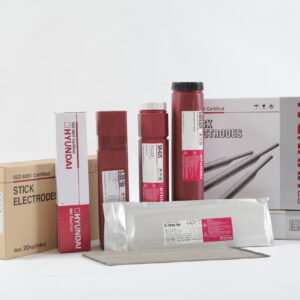
FIller Metal Breakdown

S-7018.1

S-7018.1 is an iron powder low hydrogen type electrode of high efficiency used for welding 490MPa class high tensile steel. Its usability is good with direct current applications as well as alternating current applications and easy to weld in all position.
  • Welding Positions
Welding position 1GWelding position 2FWelding position 3GWelding position 4G
1G 2F 3G 4G
Welding positions PA-PG

Classification

  • AWS A5.1/ASME SFA-5.1 E7018-1
  • JIS Z 3211 E4918
  • EN ISO 2560-A E42 4 B 3 2
  • KS D7006 E5016

Approvals

ABS BV DNV LR RINA
✓ ✓ ✓ ✓ ✓

Features

  • Suitable for butt and fillet welding of thin and medium-thick plates
  • Iron powder low hydrogen electrode high efficiency
  • Good impact value at -45°C
Polarity: AC or DC+
Redrying Conditions: 300~350°C (572~662°F) X 0.5~1hr

Application Areas

  • Heavy steel fabrication
  • Low temperature strength steel
  • Offshore structure

Base Materials to be welded

Structures using 490MPa class high tensile steel, such as bridges, building, rolling stock and low temperature used for structures.

Diameter / Packaging

Diameter Length F&HF V-up/OH Packaging
2.6(3/32) 350(14) 60-90 50-80 Packet 5kg / Carton 20kg
3.2(1/8) 350(14) 90-140 80-120 Packet 5kg / Carton 20kg
4.0(5/32) 400(16) 130-190 120-170 Packet 5kg / Carton 20kg
5.0(3/16) 400(16) 180-240 150-200 Packet 5kg / Carton 20kg
6.0(15/64) 450(18) 250-300 Packet 5kg / Carton 20kg

Typical Chemical Composition of the Wire (wt%)

C Si Mn P S
0.12 0.33 1.33 0.017 0.006

Typical Mechanical Properties of All-Weld Meta

Yield MPa(ksi) Tensile MPa(ksi) Elongation % Temp °C (°F) Impact J(ft·lbs)
455(66) 561(81) 31 -45(-50) 74(55)

Other Products You May Be Interested In

Contact Us Today