FIller Metal Breakdown

S-9018.B3

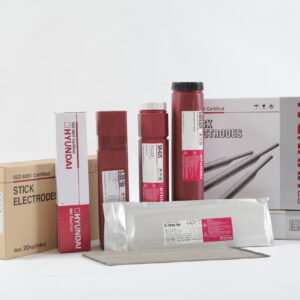
S-9018.B3 is an iron powder, low hydrogen type electrode. Its coating contains much iron powder, increasing working efficiency. Owing to this high working efficiency, it is most suitable for welding thick main pipes and steel castings.
  • Welding Positions
Welding position 1GWelding position 2FWelding position 3GWelding position 4G
1G 2F 3G 4G
Welding positions PA-PG

Classification

  • AWS A5.5/ASME SFA-5.5 E9018-B3
  • JIS Z 3223 E6218-2C1M
  • EN ISO 3580-A E CrMo2 B 3 2

Approvals

ABS DNV KR LR
✓ ✓ ✓ ✓

Features

  • Maximum service temperature at 600°C (1112°F)
  • Good mechanical properties
  • Good creep resistance
  • Iron powder low hydrogen type electrode (high efficiency)
Polarity: AC, DC±
Redrying Conditions: 300~350°C (572~662°F) X 0.5~1hr

Application Areas

  • Low alloy steel (2.25% Cr-1% Mo)
  • Pressure vessels
  • Power plants

Base Materials to be welded

Welding of 2.25% Cr – 1% Mo steel used for main steam pipes of boilers for electric power plant and marine use, equipment for oil refining industries and high temperature synthetic industries. Welding of 2.25%Cr-1%Mo steel casting.

Diameter / Packaging

Diameter Length F&HF V-up/OH Packaging
2.6 (3/32) 350 (14) 50~90 50~80 Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs)
3.2 (1/8) 350 (14) 90~130 80~120 Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs)
4.0 (5/32) 400 (16) 130~190 120~170 Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs)
5.0 (3/16) 400 (16) 190~250 – Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs)
6.0 (15/64) 450 (18) 250~300 – Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs)

Typical Chemical Composition of the Wire (wt%)

C Si Mn P S Cr Mo
0.08 0.21 0.58 0.015 0.011 2.13 1.10

Typical Mechanical Properties of All-Weld Meta

Condition Yield Strength MPa(ksi) Tensile Strength MPa(ksi) Elongation (%)
690℃*1hr 564(82) 674(98) 24

Other Products You May Be Interested In

Contact Us Today