FIller Metal Breakdown

S-7018.1H

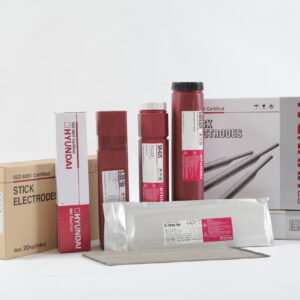
S-7018.1H is an iron powder low hydrogen type electrode. Its coating contains much iron powder, which increasing welding efficiency. Its usability is good with direct current applications and extra low-hydrogen electrode. (HDM < 4㎖/100g). Good CTOD properties at temperatures down to -10℃(14℉)
  • Welding Positions
Welding position 1GWelding position 2FWelding position 3GWelding position 4G
1G 2F 3G 4G
Welding positions PA-PG

Classification

  • AWS A5.1/ASME SFA-5.1 E7018-1 H4R
  • AWS A5.1/ASME SFA-5.1 E7018 H4R
  • JIS Z 3211 E4918 H5
  • EN ISO 2560-A E42 4 B 3 2 H5
  • KS D7006 E5016

Approvals

ABS BV DNV LR CWB CE
✓ ✓ ✓ ✓ ✓ ✓

Features

  • Extra low hydrogen electrode
  • Good impact value at -45°C
  • Vacuum sealed package available (HDM ≤ 4ml/100g)
Polarity: AC or DC+
Redrying Conditions: 350~400°C (662~752°F) X 0.5~1hr

Application Areas

  • Heavy steel fabrication
  • Low temperature strength steel
  • Offshore structure

Base Materials to be welded

Structures using 490MPa class high tensile steel, such as bridges, building, rolling stock and low temperature used for structures.

Diameter / Packaging

Diameter Length F&HF V-up/OH Packaging
2.6(3/32) 350(14) 60-90 50-80 Packet 5kg / Carton 20kg
3.2(1/8) 350/400 90-140 80-120 Packet 5kg / Carton 20kg
4.0(5/32) 400/450 130-190 120-170 Packet 5kg / Carton 20kg
5.0(3/16) 400/450 180-240 150-200 Packet 5kg / Carton 20kg

Typical Chemical Composition of the Wire (wt%)

C Si Mn P S Ni
0.09 0.25 1.27 0.017 0.005 0.02

Typical Mechanical Properties of All-Weld Meta

Condition Yield MPa(ksi) Tensile MPa(ksi) Elongation % Temp °C (°F) Impact J(ft·lbs)
As-weld 461(67) 570(83) 31 -45(-50) 100(74)
620℃*7hr 451(65) 551(80) 31 -45(-50) 82(61)

Other Products You May Be Interested In

Contact Us Today