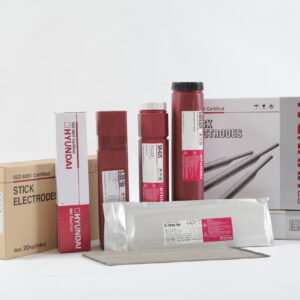
FIller Metal Breakdown

S-7018.A1

S-7018.A1 is an iron powder low hydrogen type electrode. Its coating contains much iron powder, which increasing working efficiency.
  • Welding Positions
Welding position 1GWelding position 2FWelding position 3GWelding position 4G
1G 2F 3G 4G
Welding positions PA-PG

Classification

  • AWS A5.5/ASME SFA-5.5 E7018-A1
  • JIS Z 3223 E4918-1M3
  • EN ISO 3580-A E Mo B 3 2

Approvals

Features

  • Good mechanical properties
  • Good bead appearance
  • Iron powder type electrode
Polarity: AC, DC±
Redrying Conditions: 300~350°C (572~662°F) X 0.5~1hr

Application Areas

  • Low alloy steel (0.5% Mo)
  • Pressure vessels

Base Materials to be welded

S-7018.A1 can be used for welding of 0.5%Mo heat resistant steel used for high temperature and high pressure boilers, chemical industries, oil refining industries and turbine casting. Other general low alloy steel and high tensile steel.

Diameter / Packaging

Diameter Length F&HF V-up/OH Packaging
2.6(3/32) 350(14) 55-90 50-80 Packet 5kg (11lbs), Carton 20kg (44lbs)
3.2(1/8) 350(14) 90-130 80-120 Packet 5kg (11lbs), Carton 20kg (44lbs)
4.0(5/32) 400(16) 130-190 120-170 Packet 5kg (11lbs), Carton 20kg (44lbs)
5.0(3/16) 400(16) 190-240 Packet 5kg (11lbs), Carton 20kg (44lbs)
6.0(15/64) 450(18) 250-300 Packet 5kg (11lbs), Carton 20kg (44lbs)

Typical Chemical Composition of the Wire (wt%)

C Si Mn P S Mo
0.05 0.65 0.70 0.016 0.007 0.51

Typical Mechanical Properties of All-Weld Meta

Yield MPa(ksi) Tensile MPa(ksi) Elongation % Temp °C Impact J
525(76) 627(91) 31 620 PWHT

Other Products You May Be Interested In

Contact Us Today