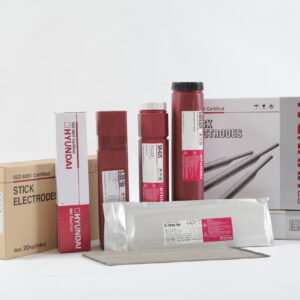

FIller Metal Breakdown


| ABS | CE |
|---|---|
| ✓ | ✓ |
| Diameter | Length | F&HF | V-up/OH | Packaging |
|---|---|---|---|---|
| 2.6 (3/32) | 350 (14) | 55~90 | 50~80 | Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs) |
| 3.2 (1/8) | 350 (14) | 90~130 | 80~120 | Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs) |
| 4.0 (5/32) | 400 (16) | 130~190 | 120~170 | Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs) |
| 5.0 (3/16) | 400 (16) | 190~240 | – | Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs) |
| 6.0 (15/64) | 450 (18) | 250~300 | – | Standard/Vacuum – Packet 5kg (11lbs), Carton 20kg (44lbs) |
| C | Si | Mn | P | S | Cr | Mo |
|---|---|---|---|---|---|---|
| 0.06 | 0.28 | 0.45 | 0.013 | 0.007 | 1.12 | 0.54 |
| Condition | Yield Strength MPa(ksi) | Tensile Strength MPa(ksi) | Elongation (%) |
|---|---|---|---|
| 690℃*1hr | 537(78) | 622(90) | 29 |